When a shipment of assembled boards arrives, the question that decides whether you accept or reject it is: does this workmanship meet the acceptance criteria in the contract? For the vast majority of electronics buyers, that criteria document is IPC-A-610, the most widely used assembly acceptance standard in the world, referenced in 3,000+ corporate and military procurement specifications. It defines, with photographs and measurement tolerances, what a good solder joint looks like, how much component damage is tolerable, and what level of cleanliness is acceptable. Without it, "defective" is an opinion; with it, "defective" is a measurement.
At Huaxing PCBA, we assemble boards to IPC-A-610 Class 2 and Class 3 on 8 SMT lines, with certified IPC-A-610 trainers performing final inspection on every lot. This guide walks you through the criteria that actually matter when you open the box, the solder joint rules, the damage limits, the contamination thresholds, plus the checklist we recommend you run at incoming inspection. If you are new to the standard family, our IPC standards comparison guide explains how A-610 fits with IPC-A-600, J-STD-001, and IPC-6012.
What IPC-A-610 Actually Governs, and What It Doesn't
IPC-A-610 is an acceptance criteria document for assembled electronic products. It answers one question: given a board that is already assembled, is the workmanship acceptable? It is deliberately visual, it uses photographs and illustrations of target, acceptable, and nonconforming conditions rather than process instructions. That is what makes it the default reference in purchase orders: a buyer and a supplier can both look at the same joint and agree on the verdict.
| Standard | Governs | Typical Use in a PO |
|---|---|---|
| IPC-A-610 | Acceptance criteria for assembled boards, solder joints, component damage, cleanliness, marking | "Assemble to IPC-A-610 Rev H, Class 2" |
| IPC-A-600 | Acceptance criteria for bare printed boards, laminate, plating, registration | "Fabricate to IPC-A-600 Class 3" |
| J-STD-001 | Process requirements, materials, soldering methods, verification | "Process per J-STD-001, Class 3" |
| IPC-6012 | Qualification/performance of bare boards, electrical, mechanical, environmental | "Qualify per IPC-6012 Class 3" |
Two practical consequences follow. First, A-610 is not a process standard, it does not tell the assembler how to solder, so it is normally paired with J-STD-001 in the same contract. Second, A-610 says nothing about the bare board itself; laminate defects, plating voids, and registration errors are judged against IPC-A-600 and IPC-6012, which we cover in our IPC-A-600 acceptance guide. When your incoming inspection flags a defect, the first step is always to identify which standard applies to that defect class.
Class 1, 2, and 3: How Acceptance Stringency Scales
IPC-A-610 defines three product classes, and the class in your contract determines the acceptance limits for every single criterion in the document:
Class 1, General Electronic Products
Consumer products where the primary requirement is function of the completed assembly. Acceptance limits are the most lenient: cosmetic imperfections that do not affect function are acceptable. Examples: disposable consumer electronics, toys, basic lighting.
Class 2, Dedicated Service Electronic Products
Products where extended life and uninterrupted service are required, but failure is not life-critical. This is the default class for most industrial, telecom, and commercial equipment. Cosmetic imperfections are acceptable if they do not affect reliability. Most commercial EMS work ships Class 2.
Class 3, High-Performance / Harsh Environment Electronic Products
Products where continued performance is critical, failure cannot be tolerated (life support, avionics, military, automotive safety). The most stringent acceptance limits in the document: no cosmetic imperfections permitted that could affect reliability, tighter fillet and damage tolerances, and 100% inspection of many criteria. Expect Class 3 to add 15-30% to assembly and inspection cost versus Class 2, driven by stricter criteria and denser inspection coverage. Our IPC Class 2 vs Class 3 guide breaks down where that cost actually goes.
The class must be written into your contract before production. You cannot "upgrade" a shipment to Class 3 after it is built, because the inspection coverage was planned around the contracted class. And note that A-610's class definitions apply to the end product: a board that goes into a Class 3 medical pump must be inspected as Class 3 even if the bare board was fabricated to a lower class.
The 5 Solder Joint Criteria That Decide Accept or Reject
Most incoming-inspection disagreements are about solder joints. IPC-A-610 evaluates every joint, through-hole, chip component, gull wing, BGA, against a small set of measurable criteria. These are the five that generate the most disputes between buyers and assemblers:
Wetting Angle: The Joint Must "Wet" the Surfaces
The solder must wet both the lead/termination and the pad, forming a contact angle of ≤ 90° between the solder and the surface. An angle greater than 90° indicates poor wetting (dewetting), which is a reject condition for all classes. This is the fastest single check a buyer can make under a microscope: glossy, concave fillets = good wetting; dull, convex, balled solder = dewetting.
Minimum Fillet Height: Solder Thickness + 25% of the Lead
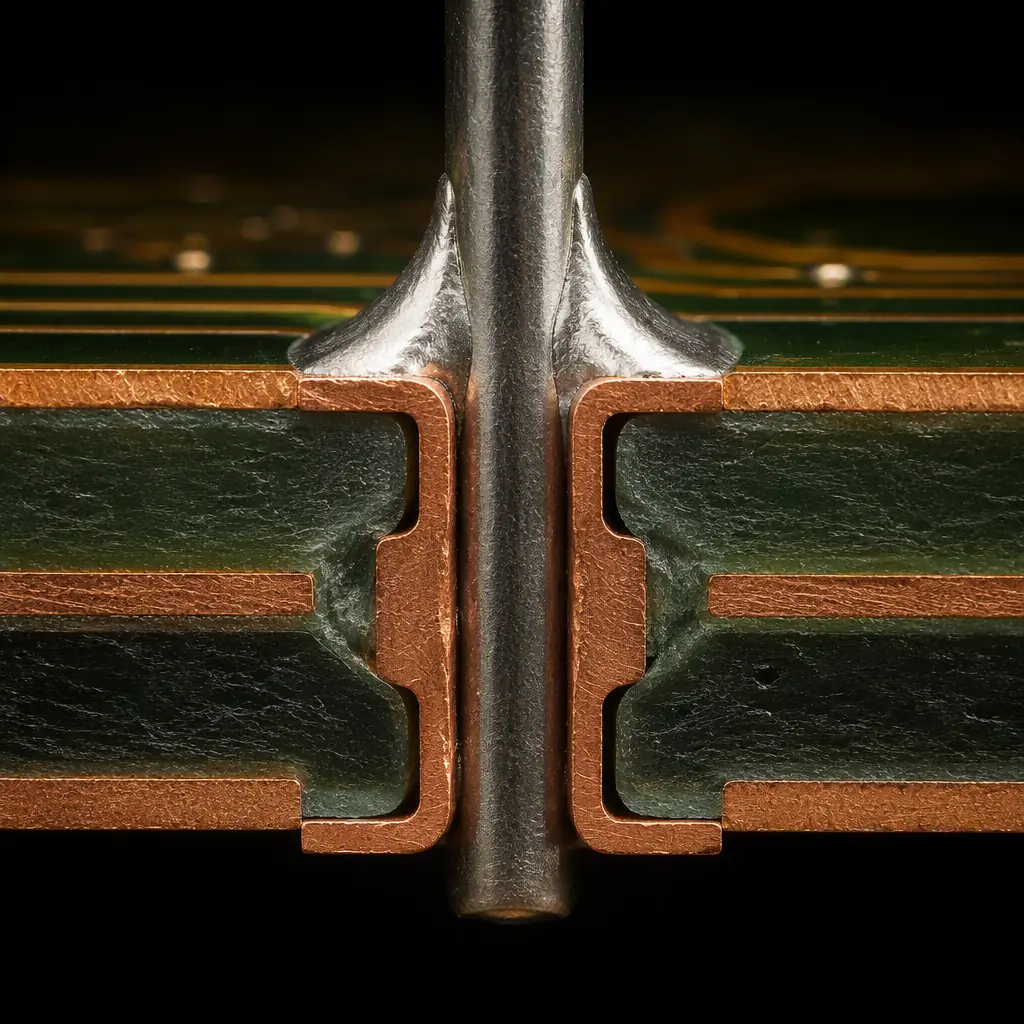
For through-hole joints, the solder fillet must extend up the lead to a minimum height of solder thickness + 25% of the lead diameter (Class 2 and 3). For chip components, the minimum fillet height is solder thickness + 25% of the termination height. A fillet that stops below this line does not guarantee a reliable mechanical and electrical connection and is rejectable.
Side Fillet Length on Chip Components: 75% of the Termination
On chip components (0402, 0201, 01005), the solder must wet along at least 75% of the termination length (Class 2), measured on the side fillet. Class 3 raises related requirements on fillet height and adds requirements for the solder to visibly wet the end cap. This is why tiny passives are the most common source of A-610 rejects, their small terminations leave little room for fillet variation. See our fine-pitch SMT assembly guide for how placement and stencil design keep these fillets in spec.
Voiding in BGA and QFN Joints: X-Ray Is the Only Way to See It
For area-array components, A-610 defers void evaluation to X-ray. The widely applied guidance (IPC-7095) caps void area at 25% of the ball cross-section for Class 2 and 15% for Class 3, with tighter limits on voids clustered under thermal pads. This criterion cannot be checked visually. Your incoming inspection must include X-ray sampling for BGA/QFN products, or you are accepting blind. Our AOI / X-Ray / SPI inspection guide covers the equipment and sampling rates.
Component Damage: Cracks Never, Chipping Within Limits
Cracks in the component body are a reject at any class. Chipping is allowed only within measured limits: for ceramic chip components, chipping must not expose the internal metallization, and total edge damage is limited to 25% of the chip's width (Class 2) with tighter limits for Class 3. Damaged components from handling, rework, or depaneling are the second most common reject category, which is why our depaneling guide emphasizes method selection as a yield issue, not just a throughput one.
Contamination and Cleanliness: The Criterion Most Buyers Forget
Solder joints are visible; ionic contamination is not, but it causes corrosion, dendrite growth, and field failures months after acceptance. IPC-A-610 requires that assembled boards be free of flux residues, oils, and other contaminants that could affect reliability. The measurable enforcement is J-STD-001's ionic cleanliness limit of ≤ 1.56 μg/cm² NaCl equivalent (for rosin-based processes requiring cleaning), verified by ROSE or ion chromatography; for no-clean processes, acceptability is judged by the A-610 visual criteria combined with surface insulation resistance (SIR) testing per IPC-9202. If your product is high-humidity or high-voltage, specify the cleanliness test explicitly in the PO. Do not assume the assembler runs ROSE by default. Our ionic contamination testing guide explains the methods and limits in detail.
Key Takeaway: The most expensive acceptance mistake is inspecting only solder joints. A board can pass every visual criterion and still fail in the field from contamination, hidden voids, or internal component damage. For Class 2/3 products, pair visual inspection with X-ray sampling and an ionic cleanliness test at first article, 3 checks that together cover what the eye alone cannot see.
How to Write IPC-A-610 Into Your Purchase Order
Acceptance criteria are only enforceable if they are in the contract. We recommend four clauses on every assembly PO:
Standard + Revision + Class, Explicitly
Write "IPC-A-610 Rev H, Class 2" (or 3), not "IPC-A-610" alone. Revisions change criteria; without a revision pin, a dispute can hinge on which edition applies. Also state the governing class of the end product, since A-610 classes describe the product, not the factory.
Deviations in Writing
Any relaxation or tightening (e.g., "X-ray void limit 20% for the thermal pad") must be a written deviation attached to the PO. Verbal allowances are unenforceable and are the #1 source of post-shipment disputes.
Inspection Data Deliverables
Require the assembler to ship the inspection records: AOI/SPI logs, X-ray reports for area-array lots, first article inspection (FAI) results, and, if specified, ionic cleanliness reports. Our FAI guide lists the documents a complete first-article package contains.
Disposition Process for Nonconforming Lots
Agree in advance on the path for rejects: 8D corrective action, sort/repair vs. scrap decision rights, return freight responsibility, and the deadline for replacement. A written disposition clause turns a quality dispute into an administrative step. Our quality dispute resolution guide covers the common clause structures.
A Buyer's 15-Point Incoming Inspection Checklist
Use this checklist when you receive assemblies. It is written to be executable by a trained inspector with a microscope, X-ray access (for area-array products), and a copy of the contracted revision:
Documentation
Certificate of conformance (CoC) states the standard, revision, class, and lot/date codes; packing list matches PO quantities.
Sampling Plan
Sample size defined in advance (e.g., ANSI/ASQ Z1.4 General Level II, AQL 1.0 for visual, 0.65 for functional), documented before inspection, not after.
Solder Joint Wetting
Spot-check wetting angle ≤ 90° on a sample of through-hole and chip joints across board quadrants.
Fillet Height
Verify minimum fillet height (solder thickness + 25% of lead/termination dimension) on through-hole and chip components.
Chip Side Fillet
Side fillet covers ≥ 75% of termination length on chip passives (Class 2).
BGA/QFN Voids
X-ray sample: void area within the contracted limit (25% Class 2 / 15% Class 3 per IPC-7095 guidance).
Component Damage
No cracks; chipping within width limits and not exposing metallization.
Misalignment
Component offset within A-610 limits (chip offset ≤ 25% of pad width for Class 2/3; no tombstoning, no skew beyond fillet coverage).
Polarity and Marking
All polarized components (diodes, electrolytics, ICs) correctly oriented; reference designators legible.
Cleanliness
No visible flux residue around joints (per A-610 visual limits for the flux type); ROSE report if contracted.
Conformal Coating
If coated: coverage, no bubbles/delamination, no coating on test points/connectors, per the coating criteria in A-610. See our conformal coating guide.
Mechanical Assembly
Connectors seated, fasteners torqued, no foreign object debris (FOD) inside the enclosure.
Electrical Test Evidence
ICT/flying probe or functional test reports included, pass rates within contract. See our testing methods guide for what each report should contain.
Traceability
Lot/date codes marked and mapped to build records, required for any product with a recall or warranty path. Our IPC-1782 traceability guide covers the data standards.
Packaging and Handling Evidence
ESD-safe packaging per the agreed standard, moisture-barrier bags with intact humidity indicator cards for MSL components, and no physical damage in transit. Our ESD packaging standards guide lists the box-level checks.
Run this checklist on first article before production, then on a contracted sampling basis per lot. For a deeper look at how to structure the incoming inspection agreement itself, sample sizes, AQLs, and hold/release authority, our incoming quality inspection guide and quality metrics guide give the benchmarks your assembler should be reporting against.
How Huaxing PCBA Implements IPC-A-610
IPC-A-610 is not a poster on our wall. It is the operating system of our quality department. Every Huaxing assembly order ships with a CoC stating the contracted standard, revision, and class. Our SMT lines run 100% AOI with 3D SPI on every printed panel, X-ray sampling on all area-array lots, and final inspection performed by IPC-A-610 certified inspectors. First articles are documented against the contracted class, and customers receive the inspection records with the shipment. If you are specifying a new product, send us your Gerber, BOM, and your class requirement. Our engineers will confirm the acceptance plan, the inspection coverage, and the criteria that apply to your specific component mix before production starts, and return a quote with the full acceptance criteria mapped to your contract.
Send your assembly files and class requirement to our quality team for a 24-hour quote with the IPC-A-610 acceptance plan included.