
Test coverage gets discussed as if it were a property of the tester. It is not. It is a property of the layout. A flying probe can reach any copper it can touch, an ICT fixture can reach any node that has a pad large enough and clear enough to land a probe on, and once the board is released, the moment for both decisions has passed. What you get afterwards is whatever the layout left behind.
The measured constraint is area. Exposing a full net list at the density a bed-of-nails fixture needs consumes between 8% and 18% of usable board area on a typical dense assembly, and that number rises sharply as pitch falls. This page works through that arithmetic, the mechanical limits that sit behind it, and the pattern of what happens to coverage when access gets negotiated away.
How Many Test Points Should a PCB Have?
The practical rule: expose every net that carries a power rail, every net on a connector, every net between two ICs where a rework joint would be unverifiable, and every node needed to isolate the functional blocks during FCT. On a mixed-signal industrial board that usually lands between 60% and 85% of all nets. Trying to reach 100% is counterproductive, because the last 15% are typically short, low-impedance nets between components that a probe cannot discriminate anyway.
| Board class | Nets exposed | Typical point count | Achievable structural coverage |
|---|---|---|---|
| Consumer control board, 0603 and above | 30 to 45% | 80 to 150 | 75 to 85% |
| Industrial control, mixed pitch | 60 to 75% | 250 to 600 | 88 to 93% |
| Automotive ECU, 0.5 mm pitch | 75 to 85% | 600 to 1,200 | 92 to 96% |
| Large FPGA board, 0.8 mm BGA | 40 to 60% accessible only | 800 to 2,000 | 70 to 85% plus boundary scan |
The last row explains why boundary scan exists. When a large BGA is surrounded by decoupling and the escape routes are dense, most of its nets can never reach a test pad. The achievable coverage for that region comes from JTAG rather than from probes, and the two are additive only if the boundary-scan chain itself has been designed in. The test-side view of how those numbers are computed is in ICT test coverage percentage audit.
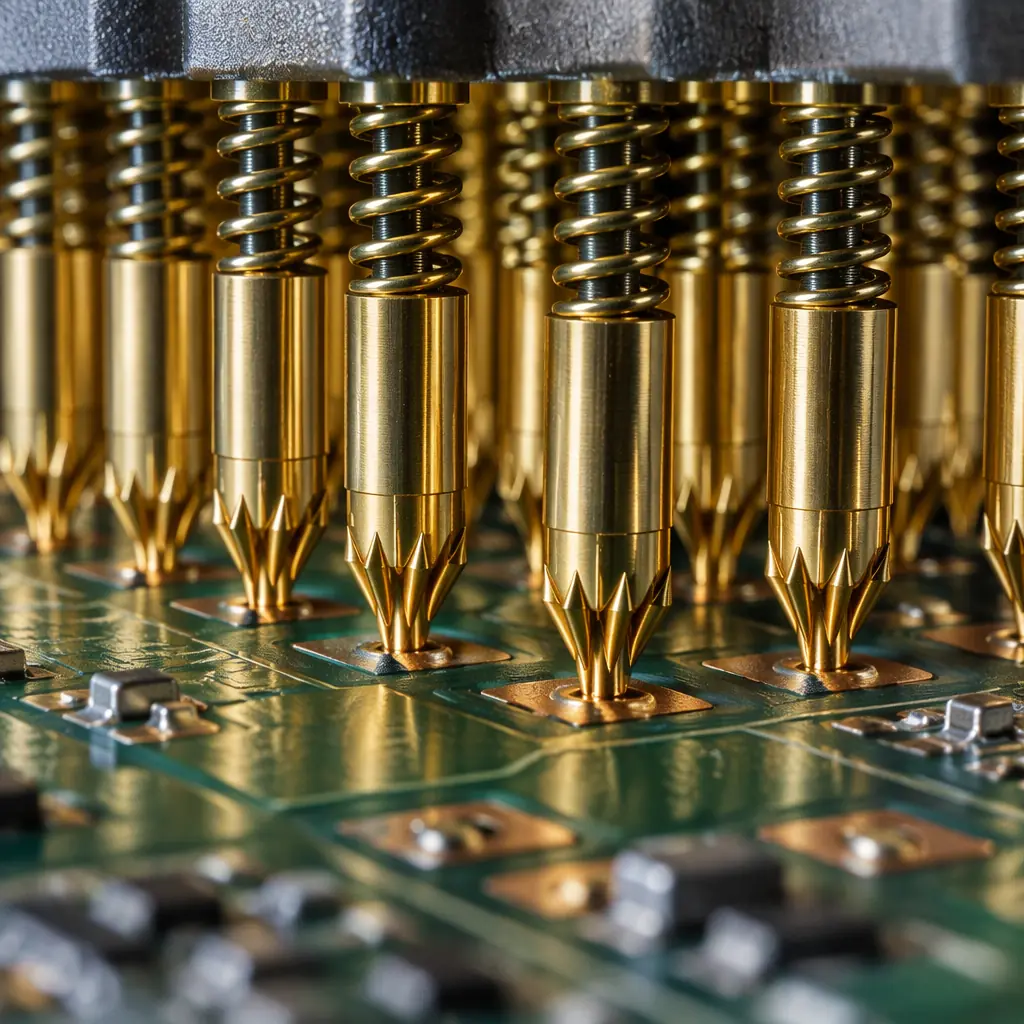
The Area Arithmetic Nobody Runs
A test pad of 0.9 mm diameter on a 1.27 mm grid, with 2.54 mm spacing to neighbours and 1 mm clearance from components, occupies roughly 2.6 mm² of keep-out once the probe-side mechanical clearance is included. A 600-point design on a 120 by 160 mm board therefore needs about 1,560 mm², or 8% of the board, before the routing cost of fanning those nets out is counted. Fanout typically doubles it.
| Parameter | Value | Consequence |
|---|---|---|
| Test pad diameter | 0.9 mm minimum, 1.0 mm preferred | Below 0.7 mm the probe crown lands off-centre and contact resistance drifts |
| Solder mask clearance per side | 0.05 to 0.1 mm | Mask shadow is the most common cause of intermittent probe contact |
| Grid pitch | 1.27 mm standard, 2.54 mm with probe guides | Fine grid needs a dedicated guide plate; cost follows |
| Component keep-out | 1.0 mm from tall parts | Probes tilt, and a tilted probe contacts the trace not the pad |
| Area per accessible net | ~2.6 mm² of keep-out | 600 points on 19,200 mm² board = 8%, doubling with fanout |
The arithmetic matters commercially because it determines the fixture, and the fixture determines the NRE. Node count drives pin count, pin count drives wiring and drilling burden, and below a defined volume the NRE never amortises. That break-even point is worked through in ICT fixture NRE and break-even volume. Choosing flying probe instead removes the fixture cost entirely but multiplies test time per board, so the two are substitutes at the wrong volume and complements at the right one.
The Probe Force Budget
Every probe presses down. A spring probe on a 1.27 mm grid carries a working force of roughly 2 to 3 N at specification compression. A 600-point fixture therefore applies about 1.5 kN, close to the weight of a small car, distributed across the board. The board has to survive that without flexing into the shadow of its own stiffeners, and the fixture has to keep the probes aligned while it does so.
| Point count | Total probe force | What it demands of the design |
|---|---|---|
| Under 200 | Under 0.5 kN | Two support posts, no stiffener |
| 200 to 600 | 0.5 to 1.5 kN | Support in the fixture, watch thin-board flex over 1.6 mm spans |
| 600 to 1,500 | 1.5 to 3.5 kN | Stiffener or thick core, deflection budget under 0.1 mm |
| Over 1,500 | Over 3.5 kN | Board stiffness is a design input, not an assembly afterthought |
The failure mode this creates is quiet. A board that flexes a third of a millimetre across its centre will contact every probe, pass, and then develop micro-cracks at the base of a BGA over the following weeks. This is why high-point-count assemblies need a mechanical review before release, and why asking the assembly house for a deflection number is more useful than asking whether the fixture is new. The same board-flexure mechanism drives the microvia reliability failures described in microvia reliability and IST testing.
What Gets Stripped, and What It Costs
Access is rarely removed deliberately. It gets removed because something else needed the space, and the trade-off was made by whoever opened the layout last. The four usual removals, and their coverage cost:
RF and antenna keep-out
Copper near a 2.4 or 5 GHz antenna degrades radiation, so all test pads inside the keep-out are removed. Typical cost: the whole RF front end drops out of structural coverage and has to be covered by functional test with a conducted or radiated measurement instead. That requires a connector in the design, and the connector decision usually comes too late.
Thermal vias and heat-spreader areas
Under a power device, every square millimetre of copper is thermal budget. Removing 40 test pads for thermals costs roughly 3 to 5 points of structural coverage directly under the device, which is the region most likely to develop voids. The mitigation is to keep the pads and connect them to the thermal plane deliberately, which is what the design practice in thermal via array design already does.
Harsh environment and coating
A conformally coated board can still be probed, but the pad must be masked or the probe must pierce the coating, and neither is free. On Parylene-coated assemblies the test sequence has to run before coating, which means the boards are tested, coated, and shipped without a second electrical gate. For products where that gap matters, the answer is a coated-board probe plan rather than no test at all, discussed in Parylene thickness and masking verification.
Density pressure from fine-pitch parts
As pitch falls below 0.4 mm, the escape routing from the component occupies the space where test pads would go. The net effect on a dense board is that accessible nodes cluster toward the perimeter and power distribution, while the interesting signal nodes disappear. This is the case boundary scan was invented for, and it has to be designed in at schematic stage, not retrofitted.
What to Settle Before Design Release
Five decisions, all of which are cheap at schematic review and expensive after ECO:
| Decision | Set it by | Cost if deferred |
|---|---|---|
| Target coverage percentage and which defect classes it must catch | Schematic | Fixture built for the wrong node set |
| Test pad size and which nets are exposed | Layout review | Fixture NRE paid twice |
| Boundary-scan chain and connector access | Schematic | Large BGA uncovered permanently |
| Whether FCT needs a board-edge or connector interface | Mechanical design | Flying leads on every unit, slow and unreliable |
| Coating versus test sequence | Process route | Ship without electrical gate, or mask and de-mask |
The commercial argument for settling these early is simple. Fixture NRE, probe replacement, and test time are all driven by decisions taken in the first two weeks of the design. Once released, each change triggers a fixture rebuild rather than a design edit. The coverage planning method that ties all of this to the product's failure modes is in PCBA test strategy and coverage planning, and the fixture cost structure is in PCBA test fixtures, ICT and FCT cost.
What We Commit to at Quote Stage
Send the Gerber and the net list and we return three numbers before an order exists: the accessible net count from your existing pads, the achievable structural coverage at that access level, and the fixture cost and lead time that follow. If the achievable coverage is below the level your failure-mode analysis requires, we say so and name the specific nets to expose, rather than building a fixture that cannot catch the defect you care about.
Frequently Asked Questions
What size should test pads be? 0.9 mm diameter minimum and 1.0 mm preferred, on a 1.27 mm grid, with at least 0.05 mm mask clearance per side. Below 0.7 mm contact resistance becomes unstable across the fixture's life and false failures climb.
Can vias be used as test points? Only if they are not tented, are at least 1.0 mm outer diameter, and are not via-in-pad on a thermal plane where the probe would sit over a void. Untented vias on a 0.6 mm diameter are a common false-failure source and are usually better replaced with a real pad.
Is flying probe a substitute for test points? It removes the fixture, not the requirement. Flying probe can land on smaller features and tolerates tighter spacing, which recovers some access, but it tests one board at a time and its economics only work below a few hundred units. The comparison is in flying probe versus ICT versus functional test.
How much board area do test points really cost? Roughly 2.6 mm² of keep-out per accessible net at 1.27 mm grid, so 600 points on a 120 by 160 mm board is about 8% of area, effectively 16% once the fanout routing is counted.
What if the design has no room for test pads? Then coverage comes from boundary scan, from a designed-in connector for functional test, or it does not come at all. All three have to be decided before release, and the cheapest is almost always the connector.
